About 100 MT Blue Star Cold Room
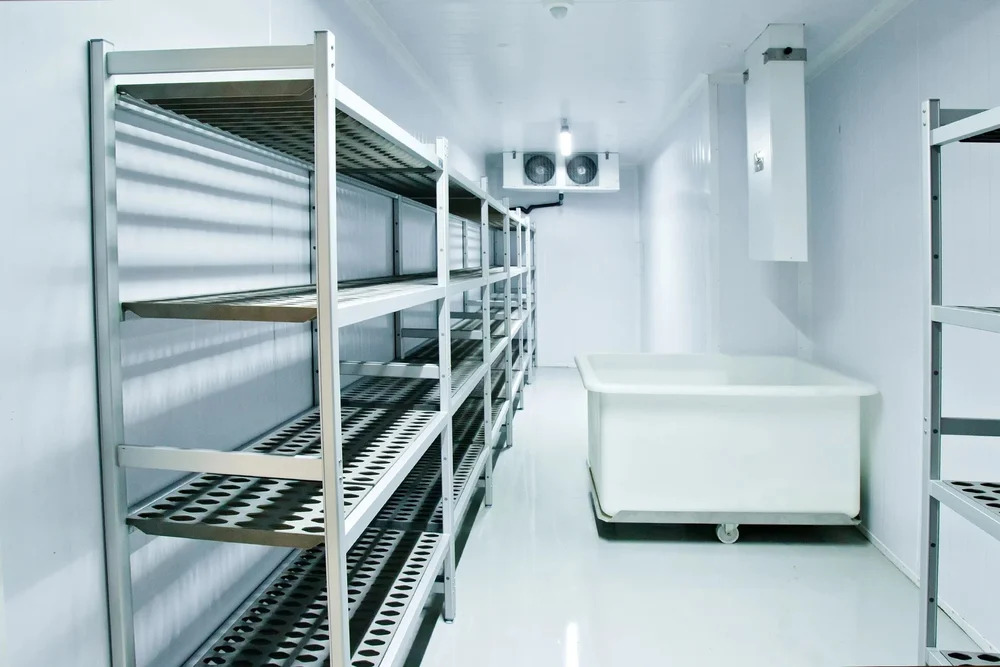
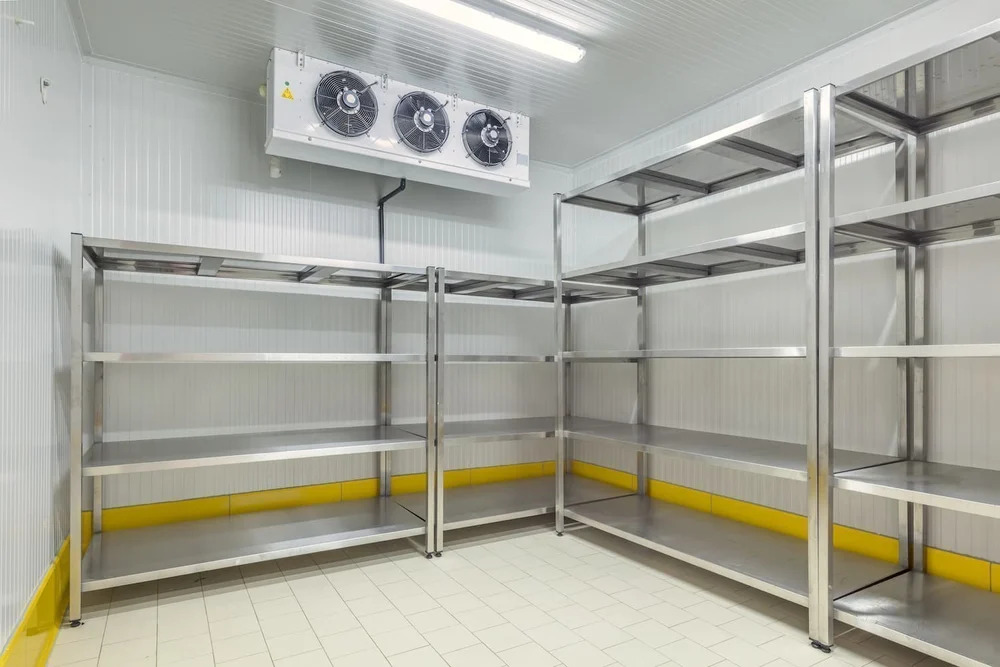
Presenting the 100 MT Blue Star Cold Room-an enviable solution offering preeminent performance in cold storage. Find value in this hot deal designed for those with transcendent storage demands, suitable for food, dairy, pharma, and more. Tailored to your requirements, the air-cooled system with PUF panel insulation and digital control maintains optimal temperatures between -20C to -25C. Heavy-duty shelves, eco-friendly refrigeration, and smooth stainless steel interiors ensure reliability, easy cleaning, and durability. The anti-slip floor, LED lighting, and automatic humidity control create a safe, energy-efficient environment. Available across India through top manufacturers, importers, and suppliers.
Versatile Plant Applications and Enhanced Features
The 100 MT Blue Star Cold Room is built for versatile use in food storage, ice cream, fruits, vegetables, pharmaceuticals, meat, poultry, and dairy sectors. Its standout features-automatic humidity control, digital display, heavy-duty racking, and customizable PUF panel insulation-make it suitable for diverse applications. Thanks to the transcendent shelving capacity and robust anti-slip flooring, this cold room elevates operational safety and storage efficiency in any commercial plant environment.
Domestic & International Dispatching and Sample Availability
With an extensive outlay in both Indian and South Asian markets, Blue Star's cold rooms are available for prompt dispatching worldwide. We streamline order processing for bulk and custom requirements, ensuring fast outflow to key export destinations. Customers benefit from samples available on request. Serving both main domestic markets and established export partners, our supply network guarantees timely, reliable, and efficient delivery wherever you operate.
FAQ's of 100 MT Blue Star Cold Room:
Q: How does the Blue Star Cold Room benefit pharmaceutical and food storage applications?
A: The Blue Star Cold Room provides strict temperature and humidity control, ensuring preservation of pharmaceuticals, frozen foods, fresh produce, and dairy products under optimal conditions to maintain quality and safety.
Q: What makes the maintenance process of this cold room easy and efficient?
A: The smooth interior finish, stainless steel body, and easy-to-clean design facilitate regular maintenance, while the anti-slip floor and digital control panel simplify operation and upkeep.
Q: Where can this walk-in cooler be used most effectively?
A: It is ideal for use in food processing units, laboratories, supermarkets, dairy plants, and pharmaceutical storage areas, offering reliable temperature control and storage adaptability.
Q: What are the steps involved in order processing and dispatching this product?
A: Once an order is received, we consult on requirements, customize the size and panel thickness, then expedite manufacturing. After quality checks, the finished cold room is promptly dispatched for installation and operation.
Q: When is sample availability possible for this cold room model?
A: Samples or on-site demonstrations can be arranged upon request, subject to scheduling and outlaying specifics at your location.
Q: How is energy efficiency achieved in this cold room?
A: The air-cooled system, eco-friendly refrigerant, LED lighting, and automatic humidity control collectively reduce power consumption, ensuring cost-effective and environmentally sound operation.

 Send Inquiry




 Send Inquiry


 Send Inquiry
 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
